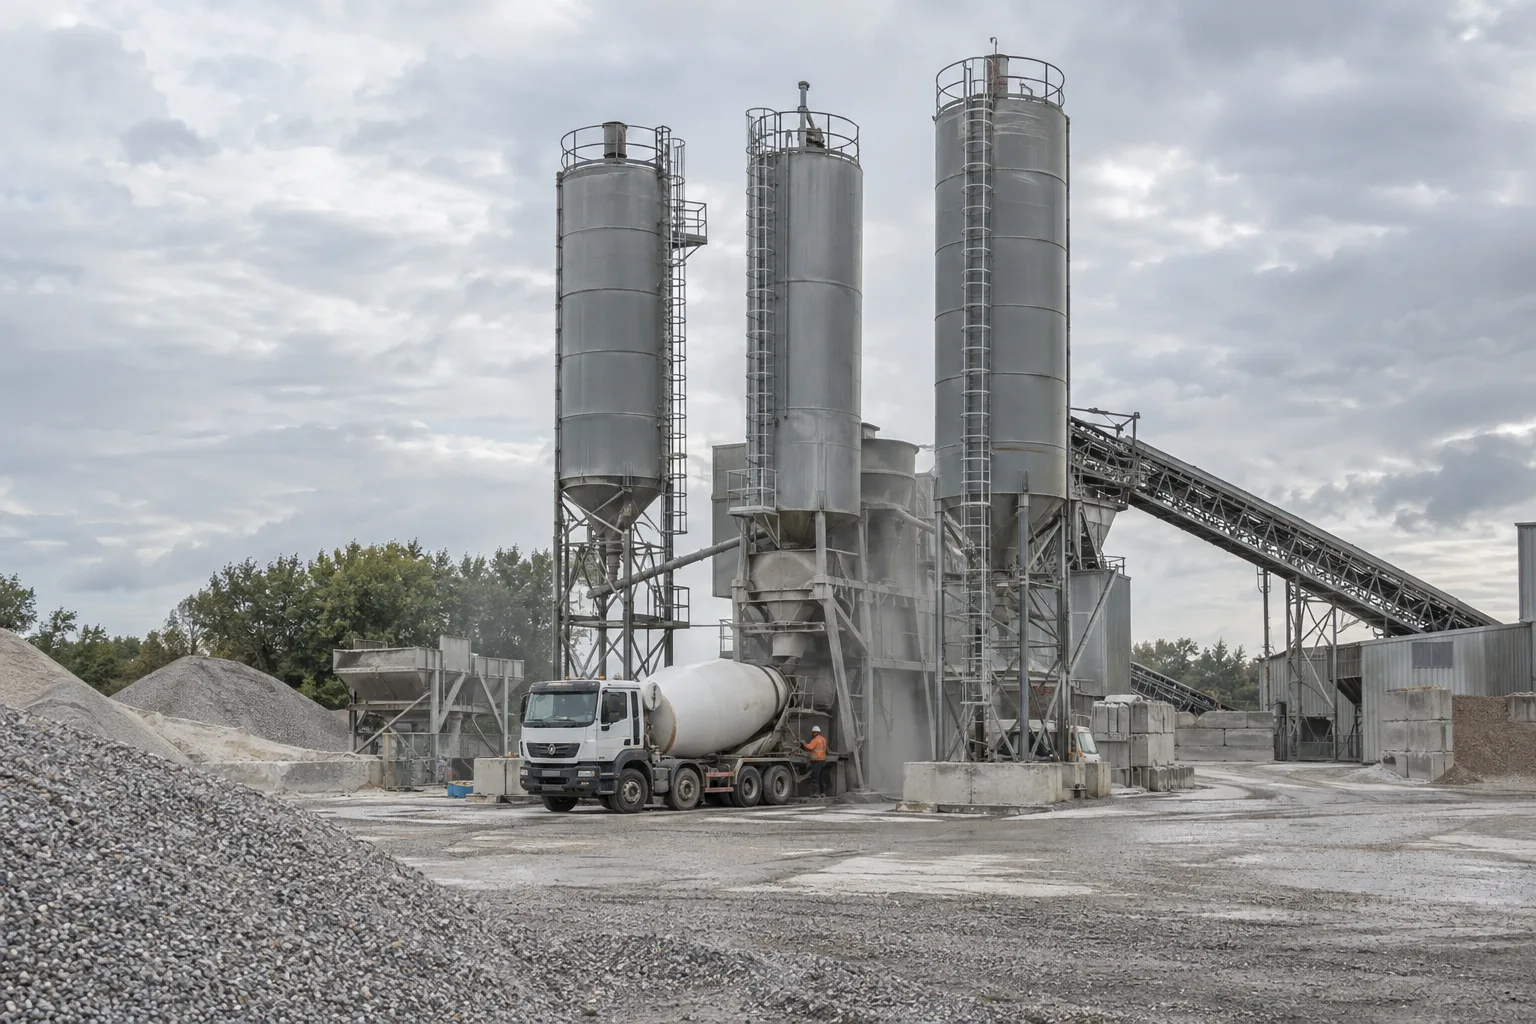
Cement is one of the hardest materials to measure the level of. It arrives through a pneumatic line that fills the silo with dust, it settles into a surface that reflects very little, and it sticks to anything left in its way. A cement silo level sensor has to be chosen around those three facts. The same applies to fly ash, lime, flour and the other fine dry powders that behave like cement inside a silo.
This guide covers that choice: why powder defeats some sensor types, what to look for in a radar, and how the readings from several silos become one inventory view. If you are comparing sensor families from the start, our silo level monitoring overview covers radar, ultrasonic, load cells and capacitive sensors side by side.
Why cement and fine powders are hard to measure
Dust arrives with every delivery. Cement is blown into the silo from the tanker. For the whole of the fill, and for some time afterward, the space above the product is an opaque cloud. Any sensor that depends on a clear path through air struggles at exactly the moment a delivery needs to be confirmed.
Fine dry powder reflects weakly. Radar measures by bouncing a signal off the surface. Coarse, dense material gives a strong return. Fine, dry, aerated powder gives a faint one, and freshly delivered cement is at its most aerated right after filling. The sensor has to be built and configured for a weak echo.
Powder sticks. Cement and lime cling to walls, ladders, braces and anything mounted inside the silo. A sensor with a moving part, or one that sits in the product, gathers buildup until it stops working. Buildup on the walls also produces echoes that are not the surface.
The silo is tall, narrow and made of steel. Batch plant silos are deep cylinders full of weld seams, fill pipes and internal fittings. A wide measurement beam catches all of them. Steel walls reflect radar well, so a beam that touches the wall returns a strong signal from the wrong place.
The surface is not level. Powder fills into a cone and empties into a funnel. A single point on that shape is an approximation of the volume, so the point has to stay the same from one reading to the next.
Radar, ultrasonic, load cells or paddle switches
There are four realistic options for a cement silo, and they do not answer the same question.
| Sensor type | What it tells you | How it copes with powder |
|---|---|---|
| Rotary paddle switch | Product has reached one fixed height | Works, but a moving part in powder needs regular attention and gives no level between points |
| Ultrasonic | Continuous level | Loses its echo in the dust cloud during and after filling |
| Load cells | Weight of the silo contents | Unaffected by dust; fitting them under an existing silo is a structural job |
| 80 GHz radar | Continuous level | Reads through dust, no contact with the product, narrow beam for tall silos |
Paddle switches are the traditional fitting and still have a place as an independent high-level alarm. What they cannot do is tell you how much cement you have, how much a delivery added or when you will run out. For that you need a continuous measurement.
Load cells give true weight, which is their real advantage, and our load cells vs radar comparison covers when that is worth the installation. For most batch plants and mills the question is inventory, and a radar fitted through a roof nozzle answers it without touching the structure.
What to look for in a radar for powder
- 80 GHz with a narrow beam. The RLM-120 radar level sensor operates at 76 to 81 GHz with a 3 degree beam, and an 8 degree variant for shorter, wider vessels. In a deep cement silo the narrow beam reaches the surface without touching the wall or the fill pipe.
- A setting for low-reflectivity material. The RLM-120 has a solid media mode with separate medium settings for chunk, granular and dust-like material. Cement, fly ash and flour belong on the dust setting, which is the one meant for weak echoes.
- Tools for false echoes. A steel silo with internal fittings always returns some echoes that are not the product. The RLM-120 provides false echo learning to mask fixed obstacles, a configurable blind zone for anything near the sensor, and echo lock to keep the measurement on the true surface.
- A range that fits the silo. Variants cover 15 m, 35 m, 85 m and 120 m. The datasheet guidance is to set the range about 2 m beyond the vessel height so the sensor sees a complete echo. A batch plant silo normally needs one of the two shorter variants.
- No contact and no moving parts. The lens antenna sits at the top of the silo, above the product. Nothing dips into the powder, so there is nothing for cement to seize.
- Outputs that fit what you already have. 4-20 mA and RS485 Modbus are both provided, so the sensor connects to an existing plant PLC or to an IoT controller without a converter.
- Damping you can set. A powder surface moves during filling and discharge. Adjustable damping time smooths the reading so the trend reflects the average level and not every slump in the cone.
From single silos to plant inventory
One reading answers “how full is this silo”. A batch plant or a mill usually has several, holding different products, and the useful question is what is on site in total and what needs ordering.
- Each silo carries its own radar. The sensors connect over RS485 Modbus to an Omni Genesis controller, which has four modular sensor ports, so neighboring silos share one controller.
- The controller transmits over cellular (4G LTE). The silo group needs no network cable to the office, which matters on plants where the silos stand across a yard from any building.
- The cloud dashboard shows every silo side by side: current level, each delivery as a visible step, consumption between deliveries, and a low-stock alert per silo.
That turns ordering into a threshold event. It also gives a record of what each delivery added, which is otherwise a matter of trusting the ticket. For how the sensor, controller and dashboard fit together, see the silo monitoring solution page and our guide to how a silo telemetry setup fits together.
Installation notes for powder silos
Keep the beam away from the fill pipe. A sensor aimed into the incoming stream measures the stream. Place the nozzle so the beam lands on the settled surface, between the center of the cone and the wall.
Give it a clean nozzle. The antenna needs an unobstructed view. A long nozzle with a rough weld inside, or an edge in the beam, creates an echo right at the top of the range. Use the blind zone setting if a fixed obstacle near the sensor cannot be avoided.
Run false echo learning with the silo low. With the product level down, the sensor can record the echoes from fittings and seams, then ignore them once the silo fills.
Expect the reading to settle after a delivery. Freshly blown cement is aerated and sits higher than it will an hour later. That is the powder, not the sensor. Judge a delivery by the level after it has settled.
Calibrate volume once against a known load. Because the surface is a cone, level to tonnes is an approximation. Fix it with one delivery of known weight, and after that the differences between readings are dependable.
Conclusion
Powder punishes the wrong sensor with blind spots during filling, seized mechanisms and echoes from everything except the surface. An 80 GHz narrow-beam radar such as the RLM-120, set up for dust-like material and mounted clear of the fill pipe, gives a continuous level that survives delivery day. Connected through an Omni Genesis controller over cellular, every silo on the plant becomes a line in one inventory view.
To choose the right variant for your silos, contact us with the silo height, the product and the number of silos, or start from the silo level monitoring overview if you are still comparing technologies.